Our Factory
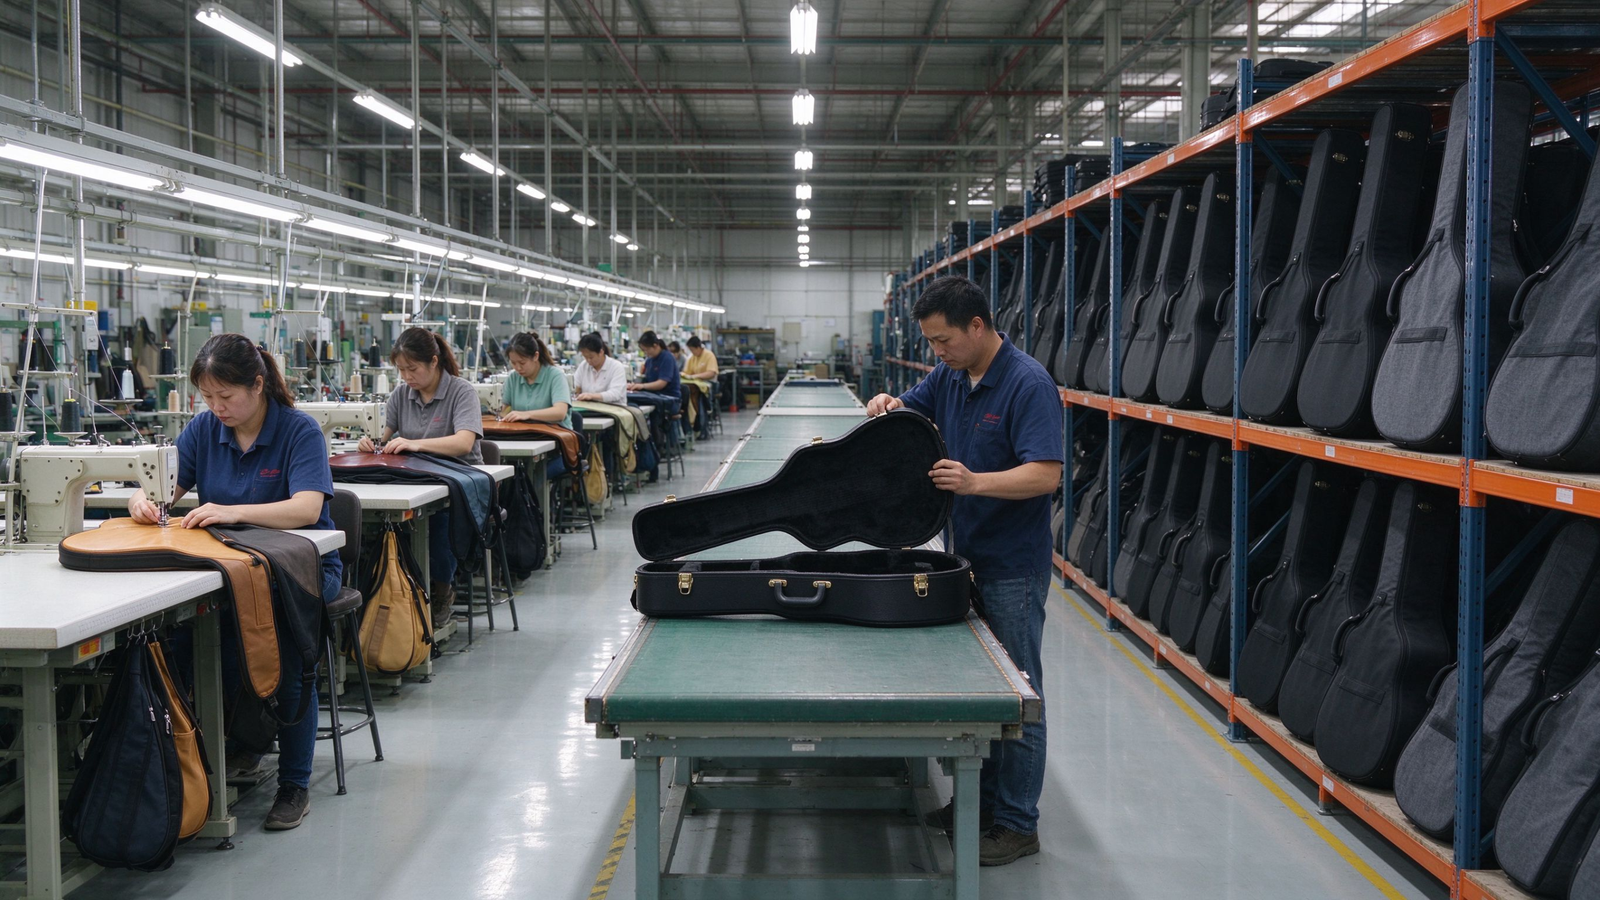
MONOGUITARBAG is a factory-direct manufacturer of instrument cases and bags. From material selection to stitching, hardware and final inspection, production happens in our own workshop – no middlemen, no subcontractors.
In-House Production
Our team of 50 skilled workers produces soft gig bags, hard-shell cases, double bags and backpacks under one roof. In-house production gives our clients full control over quality, lead time and cost, and lets us react quickly to design changes.
Materials
Our cases are made with premium PU leather, microfiber and synthetic leather, including our 1062 series materials known for durability and a rich texture. Vintage two-tone distressed finishes are available for brands targeting the European and American markets.
Design & Development
Our design team develops new models every season and supports ODM projects end to end – sketching, prototyping, sampling and production. Clients can also work with our engineers to adapt existing models to their specifications.
Certifications & Compliance
Our factory holds industry-standard quality and compliance certifications, including ISO 9001 quality management, REACH and OEKO-TEX compliant materials, and BSCI social compliance audits. Documents are available for review on request.
Quality Control
Every case is checked for stitching, zippers, hardware, padding and fit before packing. Quality control runs through each stage of production, not just at the end of the line.
Export Experience
We have been manufacturing and exporting instrument cases for over 10 years, regularly shipping to Europe and North America. We are familiar with the documentation, packing and labeling that export orders require.
Visit our OEM & ODM page to start a project, or request a quote directly.